IPC/WHMA-A-620 cable and harness manufacturing
IPC/WHMA-A-620 Cable & Harness Manufacturing Capability
Define the revision, acceptance Class and inspection plan before releasing a cable or harness drawing.
IPC 620 is a common shorthand for IPC/WHMA-A-620, a cable and wire harness assembly workmanship and acceptance standard. It covers assembly practices such as crimped and soldered terminations. Specify the standard revision and product Class in the project file. The published scope does not set in-process or end-product inspection frequency; agree sampling separately. For an EDPcable RFQ, send the drawing, BOM and acceptance requirements so process scope and evidence can be reviewed before commitment.
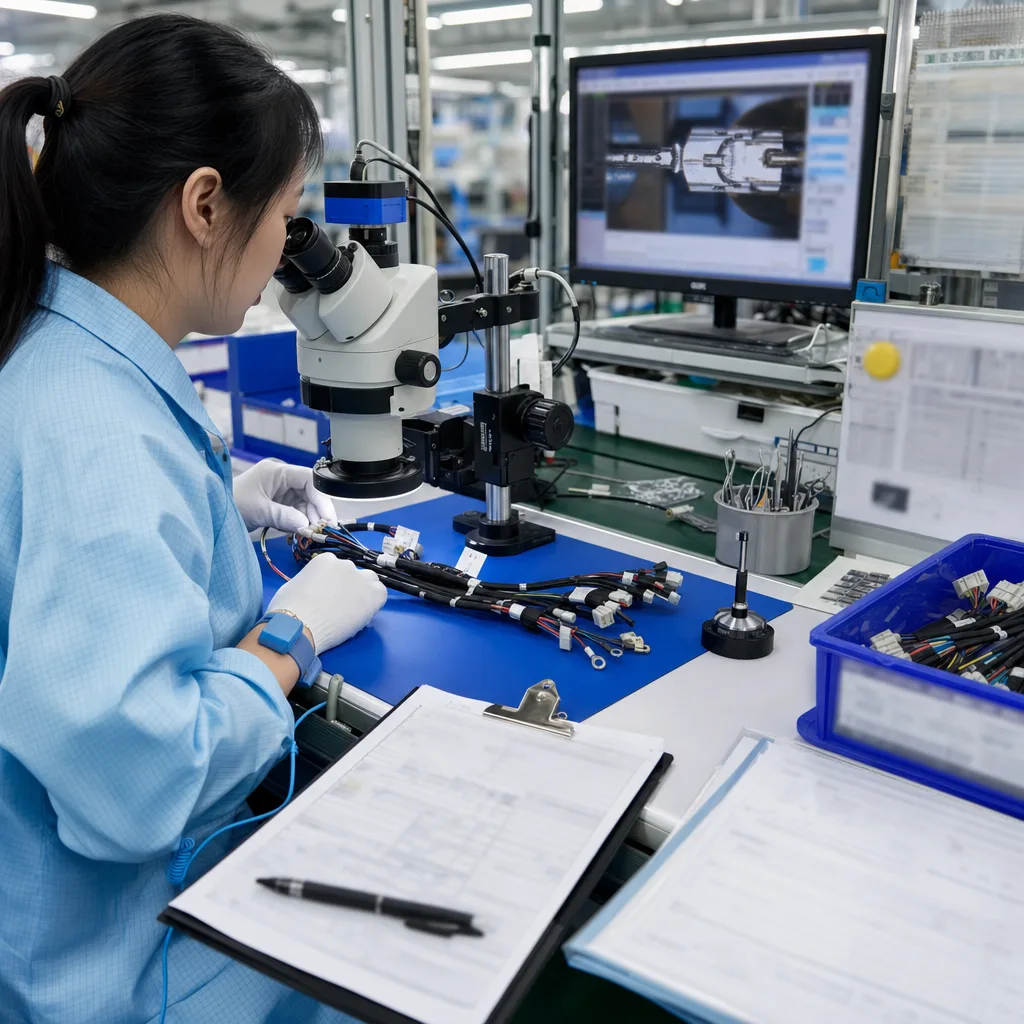
Capability scope
Use this capability when a drawing or quality agreement calls for IPC/WHMA-A-620. The standard provides the workmanship basis; the project still needs an approved pin map, component requirements and inspection plan. A Class designation alone does not establish an inspection percentage or qualify a complete device.
Name the IPC/WHMA-A-620 revision, Class and applicable customer requirements
Define visual acceptance, electrical tests and sampling as separate checks
Match requested training or qualification evidence to the person, site and process scope
Agree first-article records, lot traceability and the handling of deviations before sampling
Process Flow
| Step | Station / Action | Control Point | Output Record |
|---|---|---|---|
| Input review | Standard revision / Class / drawing / BOM / inspection plan | Resolve requirements and confirm process scope | Engineering review record |
| Training confirmation | Operator training status / training records | Trained operators matched to the Class | Training record confirmation |
| Sample build | Joining to the Class workmanship standard + internal inspection | Sample Class consistency | Sample inspection record |
| Customer sample confirmation | Customer acceptance / Class deviation discussion | Both sides confirm the release boundary | Sample confirmation record |
| Production execution | Trained operators join to the Class workmanship standard | Process Class stability | Process record |
| In-process inspection | Inspect joints using the agreed quality-plan sampling | Identify departures from applicable acceptance requirements | Inspection record with actual sampling extent |
| Release confirmation | Batch sample + IPC re-review + COC | Class + records complete | COC + IPC inspection report |
Inspection Checkpoints
Plan workmanship inspection and electrical verification separately. IPC/WHMA-A-620F, 1.1 Scope, states that inspection frequency is not specified. The following checklist is an RFQ planning aid; drawing-specific limits and the agreed quality plan control acceptance.
| Checkpoint | What to define | Evidence to request | Release boundary |
|---|---|---|---|
| Document control | Standard revision, Class, drawing and BOM revision | Approved document list and resolved requirement conflicts | Confirm requirements before selecting an inspection plan |
| Materials and tooling | Contact/wire combination, component instructions and applicable tooling | Material identifiers and applicable setup records | Class alone does not prove component or tooling compatibility |
| Termination workmanship | Crimp, solder, IDC and shield checks applicable to the design | Inspection results tied to the relevant acceptance criteria | Record actual inspection extent and agreed sampling |
| Electrical verification | Pin map, continuity/shorts and other agreed tests | Test method, limits, result and assembly or lot identifier | Electrical checks complement visual acceptance |
| Mechanical checks | Dimensions, retention, routing and strain relief as applicable | Drawing-referenced measurements or agreed test results | Do not substitute a generic force or bend limit for the design |
| Final release | Lot identity, deviations, first-article status and required records | Release record and agreed COC with supporting inspection data | Resolve nonconformances against the approved quality plan |
Deliverable Records
Request evidence for the exact assembly and lot. A supplier COC is a conformity declaration; it does not replace inspection data or establish independent site qualification. Personnel training and QML process qualification should be checked against their actual scope.
| Deliverable Record | Stage | Use | Limit |
|---|---|---|---|
| Workmanship inspection record | In-process / final | Results against the agreed revision and Class | State actual coverage; sampling follows the quality plan |
| FAI (first article inspection) | First article / pilot | Align first-article joint quality with the Class | Needs a customer-confirmed Class standard |
| COC | Production | Batch release statement | Not equivalent to third-party certification |
| Training / qualification evidence | RFQ / audit | Verify requested personnel or site/process credentials | Confirm scope, validity and disclosure terms; COC is separate |
| Batch label | Production | Trace to a specific batch + Class | Label format as agreed with the customer |
Applicable Projects
IPC/WHMA-A-620 can provide the workmanship basis for these cable families when specified in the project documents. Class, test coverage and device-level requirements are confirmed for each project:
Display interconnects: agree termination criteria and the panel-specific pin map
Medical-device harnesses: review workmanship requirements separately from device safety and regulatory evidence
Micro-coax assemblies: define termination inspection and any required signal measurements
IDC ribbon assemblies: confirm conductor/contact compatibility and termination inspection
Related Applications
IPC/WHMA-A-620 joining workmanship applies to display interconnect, medical device, FFC/FPC, IDC, LVDS, and micro-coax harness projects, and is often used together with 100% electrical testing, engineering review and drawing control, ISO 9001, and ISO 13485 medical manufacturing. When laser stripping, FPC-to-wire, or cleanroom medical harnesses are involved, the joining standard and the matching process requirements should be confirmed together.
Why EDPcable
IPC assembly requirements can be handled for display interconnect, medical device, FFC/FPC, IDC, LVDS, and micro-coax cable projects
Class requirements are reviewed before sampling so process setup and inspection records follow the same project basis
Certificate copies and training evidence can support customer audits under the agreed disclosure path
One-business-day first response, with the project team handling day-to-day quality-file coordination
FAQ
- What is IPC 620 for cable assemblies?
- IPC 620 usually refers to IPC/WHMA-A-620. It addresses cable and wire harness manufacturing practices and acceptance, including crimped and soldered connections. Use the full standard identifier, revision and required Class in an RFQ. The primary scope reference is listed below.
- Does Class 3 mean every cable must be inspected?
- The Class specifies applicable acceptance requirements. IPC/WHMA-A-620 does not set in-process or end-product inspection frequency in its scope. Define sampling or 100% inspection, lot size and response to failures in the agreed quality plan.
- Does an IPC training certificate certify the factory or cable?
- Check the exact credential and its scope. Personnel training, site/process qualification through QML, and a supplier Certificate of Conformity (COC) are different records. Request current project-relevant evidence rather than treating them as interchangeable.
- Does workmanship inspection replace electrical testing?
- Visual inspection and an electrical test answer different questions. Agree pin-map continuity and shorts checks separately; define insulation resistance or dielectric testing only where the drawing and components support the method and limits. A continuity pass alone does not establish high-speed signal performance.
- How should we specify Class 2 or Class 3?
- The customer defines the required Class and standard revision in the controlling documents, with applicable product requirements. Do not assign a Class from an industry label alone. Confirm the supplier process scope and resolve conflicting requirements before building samples.
- What documents should accompany an IPC 620 RFQ?
- Provide the controlled drawing and BOM, revision and Class, termination details, inspection and test plan, first-article requirements, record format and lot identification. State any credential or site qualification requirement explicitly so its evidence can be reviewed.
RFQ Inputs
Specify the acceptance basis and evidence needed for your cable assembly. The references below support the standard scope and credential distinctions; they do not establish EDPcable qualification or acceptance of a particular assembly. Content reviewed 9 October 2026.
| Primary reference | Source | What this reference supports |
|---|---|---|
| IPC/WHMA-A-620F, 1.1 Scope (October 2025) | https://www.electronics.org/TOC/IPC-WHMA-A-620F-TOC.pdf | Standard scope and the need to agree inspection frequency separately |
| IPC Validation Services: A-620 QML | https://www.electronics.org/validation-services-qualified-manufacturing-companies-qml-ipcwhma-620 | Site/process qualification is a distinct evidence route |
| IPC Wire Harness Assembly FAQs | https://www.electronics.org/wire-harness-assembly-faqs | Operator training and standards-based personnel certification have different purposes |
Controlled drawing and BOM, including pin map, wire/contact details and revision
IPC/WHMA-A-620 revision, required Class, addenda and customer requirements
Termination methods, component assembly instructions and process constraints
Separate workmanship inspection and electrical/mechanical test plans, including sampling, limits and failure handling
First-article and batch record formats, lot identification and agreed COC requirements
Any personnel credential or site/process qualification required, with evidence scope and disclosure arrangements
Send the IPC Class, drawing, and quality-file requirements before sampling
Confirming the Class, joining method, inspection scope, and record format early keeps samples, production, and audit documents on the same basis.